Introduction
The pharmaceutical manufacturing industry is entering a new era of transformation driven by digitalization, automation, advanced analytics, and intelligent decision-making systems. For decades, pharmaceutical production has been governed by highly controlled processes focused on compliance, quality assurance, and regulatory oversight. While traditional manufacturing models have successfully ensured the availability of safe and effective medicines, increasing market complexity, supply chain vulnerabilities, personalized medicine demands, regulatory expectations, and cost pressures are accelerating the need for a more intelligent manufacturing ecosystem.
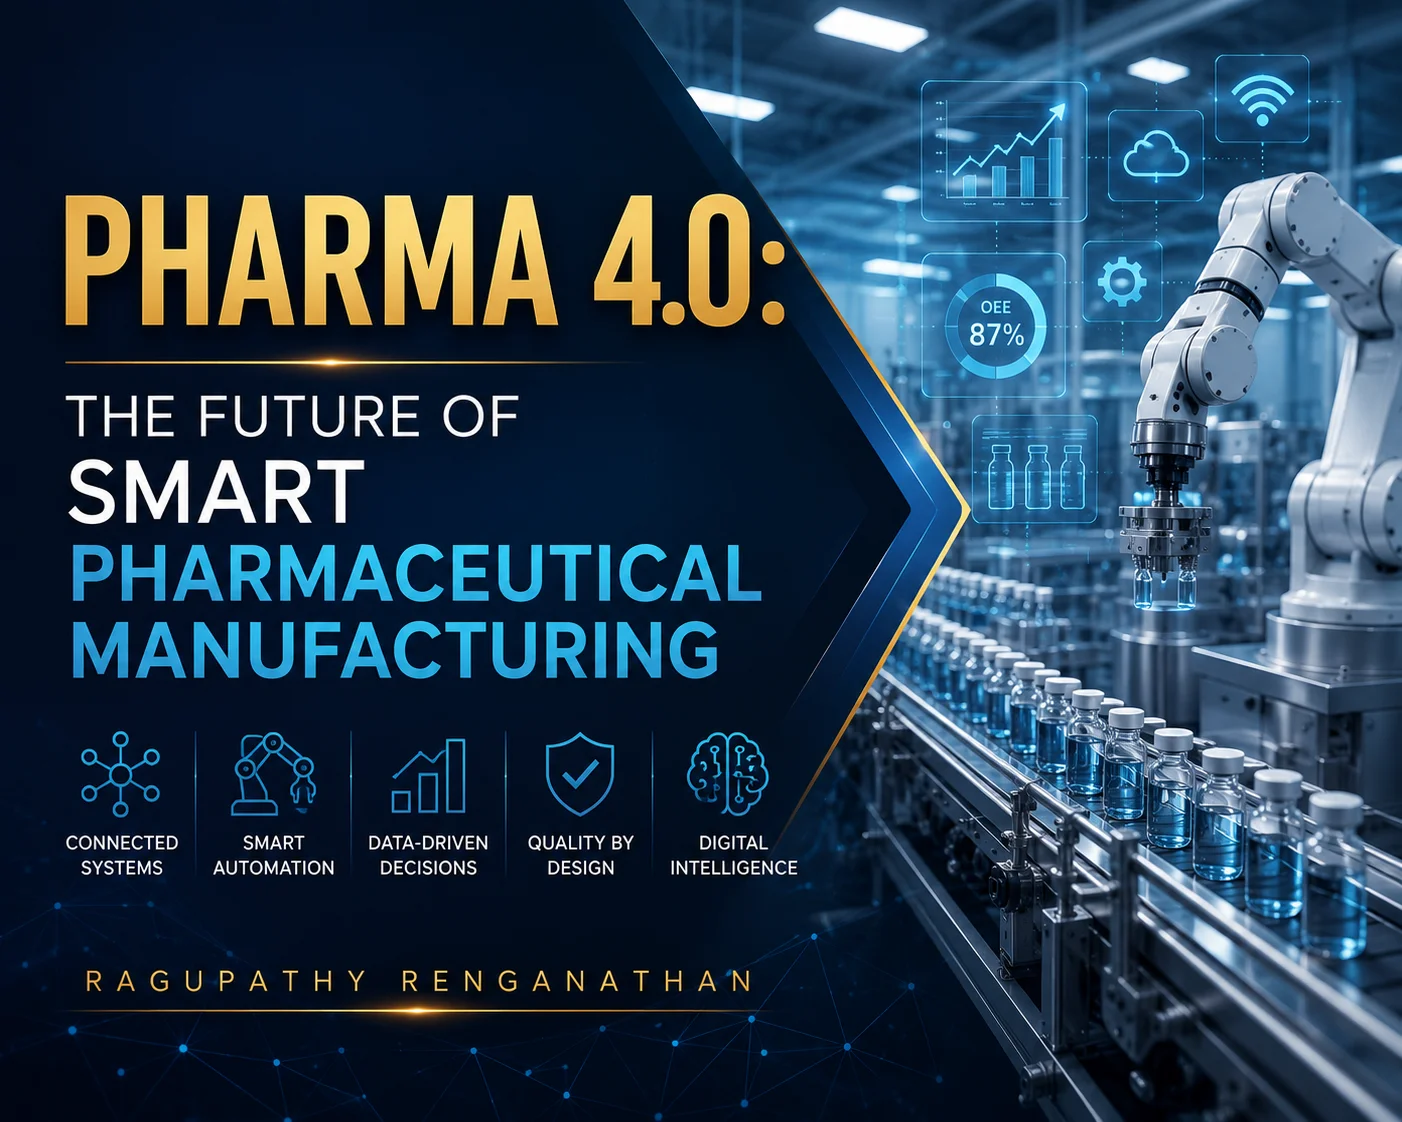
This evolution has given rise to Pharma 4.0, a pharmaceutical adaptation of the broader Industry 4.0 movement that integrates advanced digital technologies with pharmaceutical quality systems and manufacturing operations. Pharma 4.0 represents a shift from conventional automation towards interconnected, data-driven, and adaptive manufacturing environments where machines, processes, people, and information systems communicate seamlessly to optimize production performance and ensure consistent product quality.
Unlike traditional automation, which focuses primarily on controlling individual manufacturing steps, Pharma 4.0 creates an integrated ecosystem where real-time data collection, artificial intelligence, machine learning, predictive analytics, robotics, cloud computing, digital twins, Internet of Things (IoT), and advanced process control work together to enable proactive decision-making. The objective is not simply faster production but the creation of intelligent manufacturing systems capable of predicting risks, preventing failures, improving efficiency, and continuously enhancing product quality.
Regulatory agencies worldwide are increasingly supporting this transformation. The US Food and Drug Administration (FDA), European Medicines Agency (EMA), and other global health authorities recognize that advanced manufacturing technologies can improve pharmaceutical quality, strengthen supply chain reliability, and reduce manufacturing variability. Concepts such as Quality by Design (QbD), Process Analytical Technology (PAT), Continuous Manufacturing, Real-Time Release Testing (RTRT), and Quality Management Maturity (QMM) align closely with the principles of Pharma 4.0.
For pharmaceutical executives, Pharma 4.0 is not merely a technology upgrade. It represents a strategic transformation that impacts operational excellence, regulatory compliance, manufacturing agility, product quality, and long-term business competitiveness. Companies that successfully implement smart manufacturing capabilities can achieve faster decision-making, improved asset utilization, reduced waste, enhanced supply chain resilience, and greater flexibility to respond to evolving healthcare demands.
This article explores the key principles of Pharma 4.0, examines the technologies driving smart pharmaceutical manufacturing, and discusses how organizations can strategically prepare for the future of intelligent, connected, and sustainable pharmaceutical production.
Core Technologies and Principles Driving Pharma 4.0 Manufacturing
The foundation of Pharma 4.0 lies in the integration of advanced technologies with established pharmaceutical quality systems. Unlike isolated digital initiatives, Pharma 4.0 requires a holistic transformation where technology, processes, regulatory compliance, and organizational culture work together to create a highly connected manufacturing environment.
One of the most important components of Pharma 4.0 is the Industrial Internet of Things (IIoT), which enables real-time connectivity between manufacturing equipment, sensors, analytical instruments, and enterprise systems. In pharmaceutical facilities, IoT-enabled devices can continuously monitor critical process parameters such as temperature, humidity, pressure, vibration, equipment performance, and environmental conditions. This continuous flow of data provides deeper visibility into manufacturing operations and enables earlier detection of potential quality risks.
Artificial Intelligence (AI) and Machine Learning (ML) are becoming increasingly valuable in pharmaceutical manufacturing by converting large volumes of operational data into actionable insights. AI algorithms can identify patterns that may not be visible through traditional analysis, predict equipment failures, detect process deviations, optimize manufacturing parameters, and support faster decision-making. Predictive analytics allows organizations to move from reactive problem-solving towards proactive prevention of quality and operational issues.
Digital Twin technology represents another transformative capability within Pharma 4.0. A digital twin is a virtual representation of a physical manufacturing process, equipment system, or facility that continuously receives real-time data from its physical counterpart. Pharmaceutical companies can use digital twins to simulate process changes, evaluate manufacturing scenarios, optimize equipment performance, and predict the impact of modifications before implementing them in actual production environments. This reduces development risks and supports more efficient process optimization.
Process Analytical Technology plays a central role in smart pharmaceutical manufacturing by enabling real-time understanding and control of manufacturing processes. Traditional quality testing often relies on collecting samples and analyzing them after production activities are completed. PAT enables continuous monitoring of critical attributes during manufacturing using advanced analytical tools such as spectroscopy, sensors, and multivariate data analysis. This supports real-time quality assessment and strengthens process control strategies.
Continuous Manufacturing is another major pillar of Pharma 4.0. Unlike traditional batch manufacturing, continuous manufacturing allows raw materials to be continuously processed into finished products through an integrated production system. When combined with advanced process control, PAT, and digital monitoring, continuous manufacturing improves consistency, reduces production interruptions, minimizes waste, and enables faster response to market demand.